锚固件的选型与焊接要点|Selecting and Welding Refractory Anchors

摘要:衬体整块脱落追责时,锚固件是最后一个被检查的。讲锚固件材质与炉温气氛匹配、排布间距、焊接质量与涂层防护,脱落前的四个征兆。
Abstract: When a lining panel drops, anchors are the last item inspected. Matching anchor alloy to temperature and atmosphere, spacing, weld quality, coatings, and four warning signs before failure.
正文: 浇注料衬体整块掉下来,单子上写着料、施工、烘烤三项都合格。十有八九最后翻出来的是锚固件:要么材质选错被烧掉强度,要么焊缝没焊透,衬体的重量最后全由几根细杆子扛着。
Main text: When a whole castable panel drops and the report clears material, workmanship and baking, the anchor is usually the culprit: wrong alloy losing strength, or a weld that never fused — with the lining’s weight hanging on a few thin studs.
一、材质跟着温度和气氛走
1. Match alloy to temperature and atmosphere
碳钢锚固件止步于 450 摄氏度左右的背衬温度,304 不锈钢用到 800 上下,310S 能到 1050,更高温度用陶瓷锚。还原气氛和渗碳气氛会把不锈钢里的铬悄悄带走,同等炉温要往上一档选材。
Carbon steel anchors stop near 450 C backing temperature, 304 stainless works to about 800, 310S to 1050, and ceramic anchors above that. Reducing and carburising atmospheres leach chromium quietly — pick one grade up for the same nominal temperature.
二、间距与几何
2. Spacing and geometry
- 常用排布 300 到 500 毫米见方,越靠顶部与悬面越密。
Typical layout is 300 to 500 mm square, denser toward crowns and suspended walls. - 锚固件长度约为衬体厚度的一半多一点,留出热移动量。
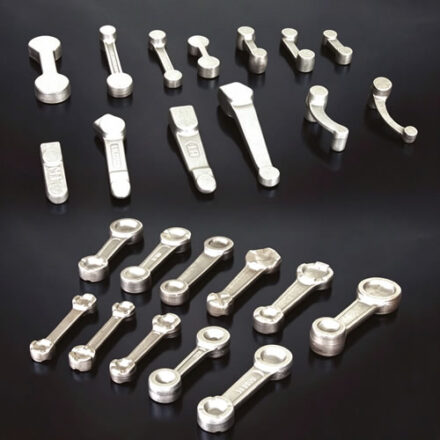
Anchor length runs a little over half the lining thickness, leaving room to move. - V 形、Y 形、L 形各有用法,双头 Y 形对平面衬最通用。
V, Y and L shapes each have their place; double-head Y suits flat panels best.
三、焊接与涂层的四条硬规矩
3. Four hard rules on welding and coating
焊缝要满焊不点焊,焊后敲渣目检;锚固件外表面缠胶带或涂蜡层,给衬体留出滑动量;氧化皮没除干净不焊;振动大的设备加角撑不要加粗杆径。衬体开裂前通常有四征兆:缝宽变宽、锚固区鼓包、温升异常、敲击声变闷,巡检时多听多看。
Weld full-fillet, never tack; chip slag and inspect. Tape or wax-coat the anchor surface to leave sliding room. Never weld over mill scale; add gussets rather than fatter studs where vibration lives. Four signs before lining cracks: widening joints, bulging over anchors, abnormal shell temperature, and a duller knock during patrol.