模锻斜度与圆角对模具寿命的影响|Draft Angles and Fillets: The Quiet Drivers of Die Life

摘要:同一副模具图纸,斜度少半度、圆角小一毫米,寿命能差三分之一。讲斜度与圆角怎么定、与脱模力和应力集中的关系、跟客户谈图纸的依据。
Abstract: On the same die drawing, half a degree less draft or one millimetre less radius can cost a third of die life. How to set both numbers, what they do to ejection and stress concentration, and how to negotiate drawings.
正文: 模具钢升级一级,寿命提两成;斜度加大半度、圆角加大一毫米,寿命常能提三成。后两者在图纸上只是两行数字,却是模具寿命最便宜的杠杆。
Main text: One steel grade up buys maybe twenty percent more die life; half a degree more draft and one millimetre more radius often buy thirty. They are two lines on a drawing — the cheapest die-life levers there are.
一、斜度的本质是脱模力
1. Draft is really about ejection force
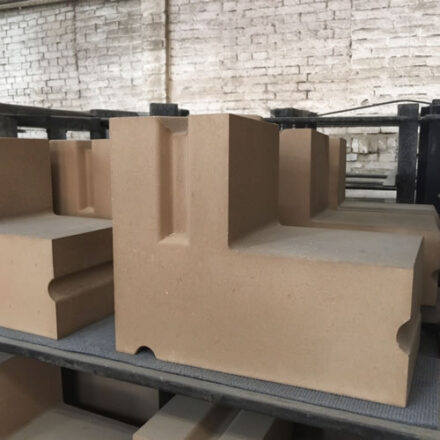
斜度不足,锻件在模膛里抱死,顶出力和顶杆载荷翻倍,顶杆断、模膛拉毛都从这里来。外斜度常规 5 到 7 度,内斜度比外斜度大 1 到 2 度,深腔件还要加。
Too little draft and the forging locks in the cavity: ejection force doubles, ejector pins snap and surfaces gall. Outside draft runs 5 to 7 degrees, inside one to two degrees more, and deep cavities need extra.
二、圆角是应力集中的开关
2. Fillets switch stress concentration on and off
- 模膛底部圆角过小,热裂从圆角根部萌生,裂纹一扩展整模报废。
Tight cavity-root fillets seed heat cracks that grow into a scrapped die. - 锻件外圆角过小,金属充填困难,折叠出现在圆角对应位置。
Tight forging fillets starve metal flow; laps appear at the matching spots. - 圆角每加大一档,充填与寿命两头受益,代价是机加工余量。
One radius class up helps both fill and life; the cost is machining allowance.
三、跟客户谈图纸的依据
3. Negotiating drawings with data
客户图纸斜度零点五度、圆角 R1,先别急着接。把同类结构的模具寿命记录拿出来摆数据:斜度加到 3 度圆角 R3,模具摊到每件的成本降多少。用成本说话,多数客户会松动。
Customer drawing calls 0.5-degree draft and R1? Do not sign yet. Put your die-life records on the table: draft at 3 degrees with R3 cuts die cost per part by how much. Lead with cost and most customers move.