耐材批次条码追溯系统的落地步骤|Landing a Batch Barcode Traceability System

Traceability projects fail at rollout, not at software. Paper first, code second, system third — and what one batch number must actually bind.
继续阅读耐材产线的能耗在线监控怎么落地|Putting Energy Monitoring on a Refractory Line
Energy is refractory's second-biggest cost after raw material, yet most shops see it only on the monthly bill. Metering granularity, unit-energy metrics and the first three dashboards worth building.
继续阅读浇注料、可塑料、喷涂料怎么选|Castable, Plastic or Gunning Mix: Choosing the Form
Three monolithic forms, three cost structures. How form follows geometry, downtime budget and the crew you actually have.
继续阅读陶瓷纤维模块炉衬怎么选型|Selecting Ceramic Fibre Module Linings
Fibre module linings heat up fast and weigh little — and leak heat where details slip. Grade choice, density, anchor system and where fibre linings should not go.
继续阅读棚板怎么选:厚度、翘曲与叠放层数|Kiln Shelf Selection: Thickness, Warping and Stacking
Shelf thickness decides payload more than kiln size does. How to match thickness to span, what warping does to stacked loads, and when cordierite-mullite or SiC wins.
继续阅读喷涂料施工的回弹控制|Controlling Rebound in Refractory Gunning
Rebound is paid-for material bouncing off the wall. What actually drives the 15 to 40 percent loss, and the settings that bring it down.
继续阅读锚固件的选型与焊接要点|Selecting and Welding Refractory Anchors
Anchors are small, cheap and blamed for nothing — until a lining panel drops. Material matching, spacing, coating and the welding details that matter.
继续阅读耐火砖砌筑的膨胀缝怎么留|Setting Expansion Joints in Refractory Brick Masonry
Brick linings fail by pushing each other apart long before they wear out. How to size and place expansion joints by material, temperature and wall geometry.
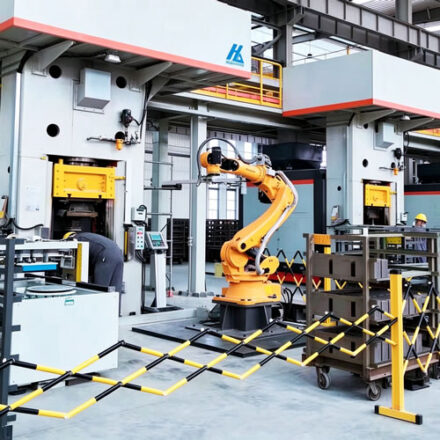
继续阅读锻压产线上下料机器人选型的四个参数|Four Parameters for Choosing a Forging Line Handling Robot
Payload and reach are the easy part. Cycle time, thermal shielding, part variance and integration depth decide whether the robot actually survives a forge shop.
继续阅读锻件加工余量和公差怎么定|Setting Machining Allowance and Tolerance on Forgings
Too much allowance wastes metal and machining hours; too little lets decarburization and oxide skin reach the finished face. How to set both numbers with a basis.
继续阅读