锻造自动化|出料热切边自动化产线改造方案与选型要点|Hot Flash Trimming Automation: Retrofit Plan and Selection

摘要:热锻生产中热切边是去除锻件飞边毛刺的关键工序,传统人工出料 + 热切边劳动强度大、高温高危、毛刺尺寸一致性差。本文讲解出料热切边自动化实现方式、机械手布局、压力机匹配、常见故障与产线改造落地注意事项。
Abstract: Hot trimming is the key step for removing flash while the forging is still hot. Manual transfer is labour-intensive and hazardous, and flash dimensions vary. This article covers the automation layout, handler selection, press matching, common faults and retrofit notes.
正文: 在热锻流水线中,锻件从锻压机完成成型之后,需要快速转运至热切边压力机完成飞边切除。传统生产模式依靠工人夹持高温锻件完成上下料,现场环境温度高,存在烫伤风险,同时人工操作节拍不稳定,飞边切除余量波动大,容易出现切伤本体、毛刺残留等问题。
Main text: In a hot forging line, the forging must move quickly from the press to the trimming press. Manual handling of 800-1200 °C parts risks burns, the takt is unstable, and flash removal varies – sometimes cutting into the body, sometimes leaving residue.
改造核心组成
Core layout
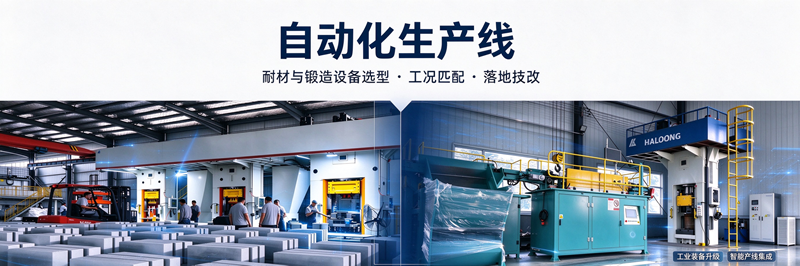
出料热切边自动化改造核心组成包含:锻机出料机械手、工件定位夹具、热切边压力机、工件定位台、废料溜槽、出料输送机构、电控联动系统。
A typical retrofit consists of the press-out handler, part locating fixture, trimming press, locating table, scrap chute, discharge conveyor and interlocked controls.
机械手选型
Handler selection
高温锻件表面温度 800‑1200℃,抓手必须选用耐高温夹爪,增加隔热防护,避免高温辐射损坏气缸与传感器;根据锻件重量选择伺服机械手或者桁架机械手,中小锻件优先桁架,大吨位锻件选用多轴机器人。
Part surfaces run at 800-1200 °C, so the gripper must be heat-resistant with thermal shielding to protect cylinders and sensors. Choose servo handlers or gantry systems by part weight: gantry for small and medium forgings, multi-axis robots for heavy ones.
工序联动逻辑
Sequence interlock
锻压机完成锻打→机械手抓取高温锻件→转运定位到热切边模具型腔→压力机执行切边→切边完成,飞边废料从溜槽排出,成品锻件取出流转下一工序。整套信号需要和锻压机、切边压力机做 IO 互锁,防止误动作。
Forging done – the handler picks the hot part, positions it in the trimming die, the press trims, flash drops through the chute and the part moves on. All signals must be IO-interlocked with both presses to prevent mis-strokes.
模具与定位
Die and positioning
自动化产线对工件定位一致性要求高,需要设计专用定位工装,补偿锻件成型误差,避免切边偏位,造成锻件损伤。
Automation demands consistent part positioning. Dedicated locating fixtures must compensate for forging tolerance so the trimming never drifts and damages the part.
改造注意点
Retrofit cautions
老旧压力机改造,需要评估原有设备行程、装模空间,不要盲目直接加装机器人;做好热防护,增加冷却风路,保护电控元器件;废料要及时排走,防止堆积卡料。
For old presses, evaluate stroke and die space before bolting on a robot. Add thermal protection and cooling air paths for the electronics, and remove scrap continuously to avoid jams.
常见问题
Common faults
抓手粘锻件、切边位置偏移、节拍跟不上锻机节奏。解决思路:优化抓手隔热与吹扫,增加工件二次定位,PLC 内部做节拍时序优化。
Typical issues: parts sticking to the gripper, trimming offset, and takt falling behind the forge press. Fixes: better gripper cooling and air purge, a secondary locating step, and PLC timing optimisation.
小结
Summary
出料热切边自动化改造,不只是简单加装机械手,需要兼顾高温工况、设备互锁、工装定位。新建产线可以一体化规划,老厂改造优先评估现有压力机硬件条件,再确定机器人与桁架方案,实现安全稳定连续生产。
Hot trimming automation is more than bolting on a robot – it must respect the heat, interlocks and fixturing. New lines can plan it as one system; retrofit shops should audit the press first, then choose robot or gantry.