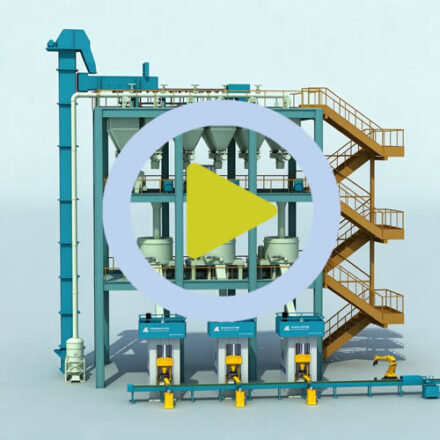
自动喷补机的成本构成与降本路径|Cost Structure and Savings Levers for automatic gunning machine


自动喷补机的问题很少单点出现,多数是参数、装备与人员三者叠加的结果。比价必须统一口径,规格、工艺与交期拉齐之后的价格才具备可比性。
一、全周期成本拆解
成本核算要区分固定投入与变动成本,把设备折旧摊进单件时容易被产量假设误导。框架协议能锁定价格,但要用质量条款约束,否则低价会被返工吃掉。
能耗在总成本中的占比常常被高估,人工与停机的隐性成本反而更大。工艺参数之间是耦合关系,单独优化一个参数常常把问题转移到下一道工序。降本要按投入产出排序,先做不花钱的管理动作,再考虑需要投资的技改。
二、主要浪费环节
备件库存是成本与风险的平衡,关键件缺货的损失远大于库存占用。成本改善的成果要能落到报表科目上,否则改善只是感觉上的。
报价单上的单价只是入口,运输、包装与损耗才是总账的差异所在。把关键参数写成可执行的作业标准,比写在总结报告里更有价值。废品率的成本影响是非线性的,靠近成品工序的废品损失远高于前段。停机一小时的成本要按整线折算,只算单台设备的损失会低估影响。
三、降本的实施顺序
选型从使用条件倒推:温度带、介质侵蚀、热震频次与机械载荷四项先定,再谈牌号。现场条件与样本实验室条件差别很大,选型结论要留出工况修正。
交付周期与售后响应要写进合同条款,口头承诺在赶工期时没有约束力。首件确认与过程巡检是两道成本很低的防线,缺了它们,返工成本会成倍上升。接口尺寸与安装空间要在选型阶段确认,装不进去的先进设备毫无意义。把总拥有成本折算到单件,比只比采购价更接近真实决策依据。
四、效果验证与固化
关键尺寸的全检与抽检要分开设计,混在一起会拖慢交付。抽检比例应随风险调整,新供应商与新批次前段的抽样密度要更高。
数据要能画出分布而不是只报合格率,分布形状才说明过程能力。工艺改善要先固定现状再做单变量试验,否则数据无法归因。判定标准中的边界值要明确处理规则,模糊地带最容易产生争议。不合格品的隔离与处置流程要演练过,真实发生时才不会乱。
五、小结
对自动喷补机而言,稳定比先进更重要,稳定之后才有条件谈效率与成本。对自动喷补机保持工艺纪律,比频繁调整参数更容易得到稳定结果。
Problems with automatic gunning machine seldom come from a single point; they are usually parameter, equipment and operator stacked together. Price comparison needs a common basis; only after specification, process and lead time are aligned is the number meaningful.
1. Breaking down life-cycle cost
Costing must separate fixed investment from variable cost; spreading depreciation per piece is easily misled by output assumptions. Framework agreements lock price, but only quality clauses stop rework from eating the savings.
Energy is often overestimated as a cost share; hidden labour and downtime costs are usually larger. Process parameters are coupled; optimising one in isolation usually pushes the problem downstream. Rank savings by payback: spend nothing on management fixes first, then consider capital projects.
2. Where the waste sits
Spare inventory balances cost against risk; a stockout on a critical part costs far more than the carrying charge. Savings must land in a ledger line, otherwise the improvement is only a feeling.
The quoted unit price is just the entry; freight, packaging and losses make the real difference. Writing key parameters into an executable work standard is worth more than recording them in a summary report. Scrap cost is non-linear: losses near the finished end far exceed those upstream. Cost downtime against the whole line; single-machine figures understate the impact.
3. Sequence for savings
Select backwards from service conditions: temperature band, chemical attack, shock frequency and mechanical load come first, grade second. Field conditions differ sharply from lab samples, so conclusions need a service-condition correction.
Put lead time and service response into the contract; verbal promises carry no weight during a schedule crunch. First-piece approval and in-process patrol are cheap defences; without them rework cost multiplies. Confirm interface dimensions and installation space during selection; an advanced machine that does not fit is worthless. Converting total cost of ownership into cost per piece comes far closer to a real decision than price alone.
4. Verifying and locking in
Design full and sampled inspection separately; mixing them slows delivery. Sampling intensity should follow risk; new suppliers and the front of a new batch need denser checks.
Report distributions, not just pass rates; the shape reveals process capability. Freeze the current state before single-variable trials, otherwise the data cannot be attributed. Define how boundary values are handled; ambiguous zones generate the most disputes. Rehearse the segregation and disposition flow for nonconforming product so it works when it matters.

