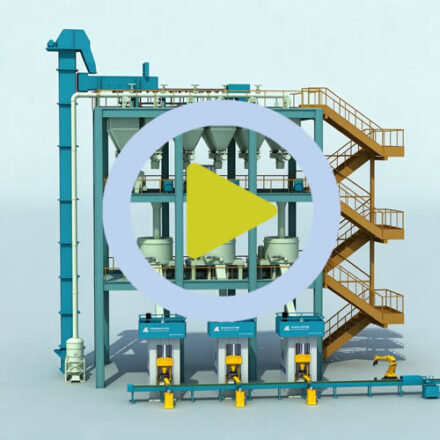
自动给料机的自动化改造与产线集成|Automation Upgrades and Line Integration for automatic feeder


自动给料机的改善投入讲究次序,先解决高频小问题,再动大改。自动化上线初期要保留人工复核,等数据稳定后再撤。
一、改造的切入顺序
自动化收益要用人均产出与稳定性两项衡量,只看减员会低估改造价值。数据采集要与改善闭环绑定,采集了不做分析,投资回报就停在报表上。
人机协作的界面设计影响接受度,操作路径超过三步就会被绕过。工艺参数之间是耦合关系,单独优化一个参数常常把问题转移到下一道工序。自动化的第一步是把人工动作写成标准节拍,动作不稳定时上设备只会放大波动。
二、数据与联锁设计
传感器漂移会悄悄改变控制结果,定期校准比增加传感器更有效。异常处理逻辑要预留人工接管入口,全自动状态下的卡料往往演变成长时间停机。
自动化改造宜分阶段推进,单工序先跑通再连成线,一次铺开的风险最高。把关键参数写成可执行的作业标准,比写在总结报告里更有价值。设备联网后首先要解决数据口径统一,各系统各说各话时集成毫无价值。自动化接口协议要在采购阶段确认,事后适配的成本远高于预期。
三、节拍与缓冲配置
把工艺卡上的参数换算成设备可执行的设定值,需要一张对照表,否则一线只能自行解释。中心值确定后仍需保留微调余量,材料批次间的吸水率差异会带来偏移。
现场习惯用经验值起步是合理的,但经验值必须被数据逐步校正。首件确认与过程巡检是两道成本很低的防线,缺了它们,返工成本会成倍上升。把关键参数做成趋势图而不是单点数值,波动趋势比瞬时读数更早暴露异常。温度与时间是同一条曲线的两端,升温快慢会改变材料内部的应力分布。
四、投入产出的测算
废品率的成本影响是非线性的,靠近成品工序的废品损失远高于前段。降本要按投入产出排序,先做不花钱的管理动作,再考虑需要投资的技改。
停机一小时的成本要按整线折算,只算单台设备的损失会低估影响。工艺改善要先固定现状再做单变量试验,否则数据无法归因。模具与工装的摊销要按实际产量算,按理论产能算会低估单件成本。把返工与挑选的人工计入质量成本,改善的必要性才容易被看见。
五、小结
对自动给料机而言,稳定比先进更重要,稳定之后才有条件谈效率与成本。对自动给料机保持工艺纪律,比频繁调整参数更容易得到稳定结果。
Sequencing matters in automatic feeder: clear the frequent small issues before committing to major changes. Keep manual review during early automation and withdraw it once the data settles.
1. Where to start
Measure automation by output per head and stability; headcount alone understates the value. Data collection must be tied to a closed improvement loop, or the return stops at a dashboard.
Human-machine interface design drives acceptance; workflows beyond three steps get bypassed. Process parameters are coupled; optimising one in isolation usually pushes the problem downstream. The first automation step is writing manual work into a standard cycle; automating unstable motion only amplifies variation.
2. Data and interlocking
Sensor drift quietly changes control outcomes; periodic calibration beats adding sensors. Leave a manual takeover path for exceptions; a jam in full-auto mode often becomes a long stop.
Automate in stages: prove one station, then link the line; a big-bang rollout carries the most risk. Writing key parameters into an executable work standard is worth more than recording them in a summary report. Once machines are connected, unify data definitions first; integration is worthless when systems disagree. Confirm interface protocols at purchase; retrofitting later costs far more than expected.
3. Takt and buffering
Turning process-card values into machine settings needs a conversion table, or the floor interprets them freely. Keep some trim authority after the centre value is fixed, since batch-to-batch water absorption shifts the optimum.
Starting from rule-of-thumb values is fine, provided the data is allowed to correct them over time. First-piece approval and in-process patrol are cheap defences; without them rework cost multiplies. Plot key parameters as trends rather than single readings; drift shows up earlier than an alarm. Temperature and time are two ends of one curve; heating rate reshapes the internal stress pattern.
4. Calculating the return
Scrap cost is non-linear: losses near the finished end far exceed those upstream. Rank savings by payback: spend nothing on management fixes first, then consider capital projects.
Cost downtime against the whole line; single-machine figures understate the impact. Freeze the current state before single-variable trials, otherwise the data cannot be attributed. Amortise tooling on actual output; theoretical capacity understates unit cost. Put rework and sorting labour into quality cost so the case for improvement becomes visible.

