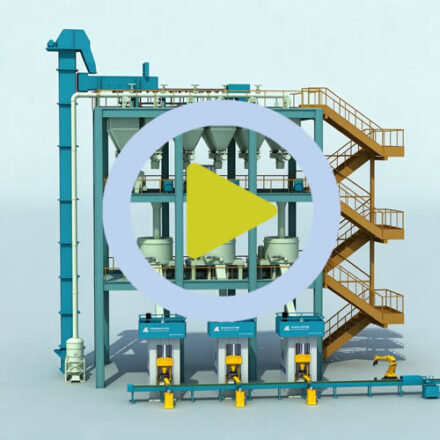
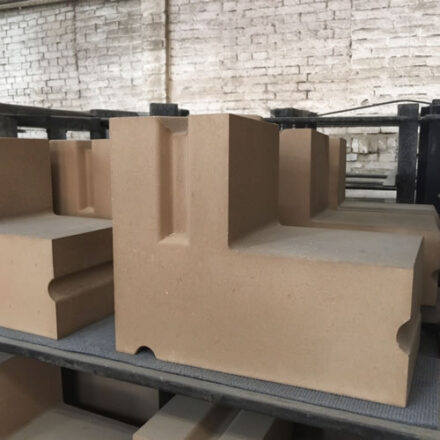
全自动液压压砖机的自动化改造与产线集成|Automation Upgrades and Line Integration for automatic hydraulic brick press


全自动液压压砖机的改善投入讲究次序,先解决高频小问题,再动大改。数据采集要与改善闭环绑定,采集了不做分析,投资回报就停在报表上。
一、改造的切入顺序
人机协作的界面设计影响接受度,操作路径超过三步就会被绕过。传感器漂移会悄悄改变控制结果,定期校准比增加传感器更有效。
异常处理逻辑要预留人工接管入口,全自动状态下的卡料往往演变成长时间停机。耐火砖的寿命由材质体系、砌体结构与升温制度三者共同决定,只比牌号容易选错。视觉检测的落地难点在样本与判定阈值,前期标注质量决定后期稳定性。
二、数据与联锁设计
自动化改造宜分阶段推进,单工序先跑通再连成线,一次铺开的风险最高。设备联网后首先要解决数据口径统一,各系统各说各话时集成毫无价值。
自动化的第一步是把人工动作写成标准节拍,动作不稳定时上设备只会放大波动。砖缝是砌体的薄弱环节,灰缝厚度与泥浆饱满度对整体气密性的影响常被低估。自动化接口协议要在采购阶段确认,事后适配的成本远高于预期。报警阈值设得太密会让人麻木,分级报警才有人真看。
三、节拍与缓冲配置
小批试产时建议同步记录环境条件,温差与湿度对结果的影响通常被低估。参数调整的幅度要设上限,超限变更应走评审,否则经验试错会累积成质量风险。
全自动液压压砖机的工艺窗口应当用上下限加中心值三段描述,只给一个推荐值在现场几乎没有可操作性。热震造成的裂纹多从工作面棱角起裂,选型时应把热震频次与抗渣需求放在一起权衡。换型后的前几件必须加密检测,参数稳定之前的判断都不够可靠。
四、投入产出的测算
能耗在总成本中的占比常常被高估,人工与停机的隐性成本反而更大。备件库存是成本与风险的平衡,关键件缺货的损失远大于库存占用。
成本改善的成果要能落到报表科目上,否则改善只是感觉上的。库存与运输的受潮、磕碰会直接降低砖坯合格率,包装与堆码规范属于质量成本的一部分。报价单上的单价只是入口,运输、包装与损耗才是总账的差异所在。
五、小结
数据完整是后续所有分析的前提,记录缺失时经验很难沉淀成规则。把全自动液压压砖机的关键动作固化成点检与首件确认,比依赖个人经验更可靠。
Sequencing matters in automatic hydraulic brick press: clear the frequent small issues before committing to major changes. Data collection must be tied to a closed improvement loop, or the return stops at a dashboard.
1. Where to start
Human-machine interface design drives acceptance; workflows beyond three steps get bypassed. Sensor drift quietly changes control outcomes; periodic calibration beats adding sensors.
Leave a manual takeover path for exceptions; a jam in full-auto mode often becomes a long stop. Brick service life is set jointly by material system, lining structure and heat-up schedule; comparing grade alone invites misselection. Vision inspection succeeds or fails on samples and thresholds; annotation quality decides long-term stability.
2. Data and interlocking
Automate in stages: prove one station, then link the line; a big-bang rollout carries the most risk. Once machines are connected, unify data definitions first; integration is worthless when systems disagree.
The first automation step is writing manual work into a standard cycle; automating unstable motion only amplifies variation. Joints are the weak link of a lining; joint thickness and mortar fullness are routinely underestimated in their effect on gas tightness. Confirm interface protocols at purchase; retrofitting later costs far more than expected. Too many alarms breed numbness; tiered alarms actually get read.
3. Takt and buffering
Record ambient conditions during pilot runs; temperature and humidity effects are usually underestimated. Cap the size of parameter changes; anything beyond it goes through review, or trial-and-error turns into quality risk.
The process window for {t} should be described as lower limit, centre and upper limit; a single recommended value is barely usable on the floor. Thermal-shock cracks usually initiate at working-face edges, so selection should weigh shock frequency together with slag resistance. After a changeover, inspect the first few pieces closely; nothing is reliable until the parameters settle.
4. Calculating the return
Energy is often overestimated as a cost share; hidden labour and downtime costs are usually larger. Spare inventory balances cost against risk; a stockout on a critical part costs far more than the carrying charge.
Savings must land in a ledger line, otherwise the improvement is only a feeling. Moisture pickup and chipping in storage and transport cut usable yield directly; packaging and stacking rules are part of quality cost. The quoted unit price is just the entry; freight, packaging and losses make the real difference.

